Oct 10, 2026CNC Machining Tips
303 vs 304 vs 316 vs 17-4: Choosing Stainless Steel for CNC Parts
303, 304, 316 and 17-4 compared for CNC parts — machinability, corrosion resistance and strength mapped to real applications.
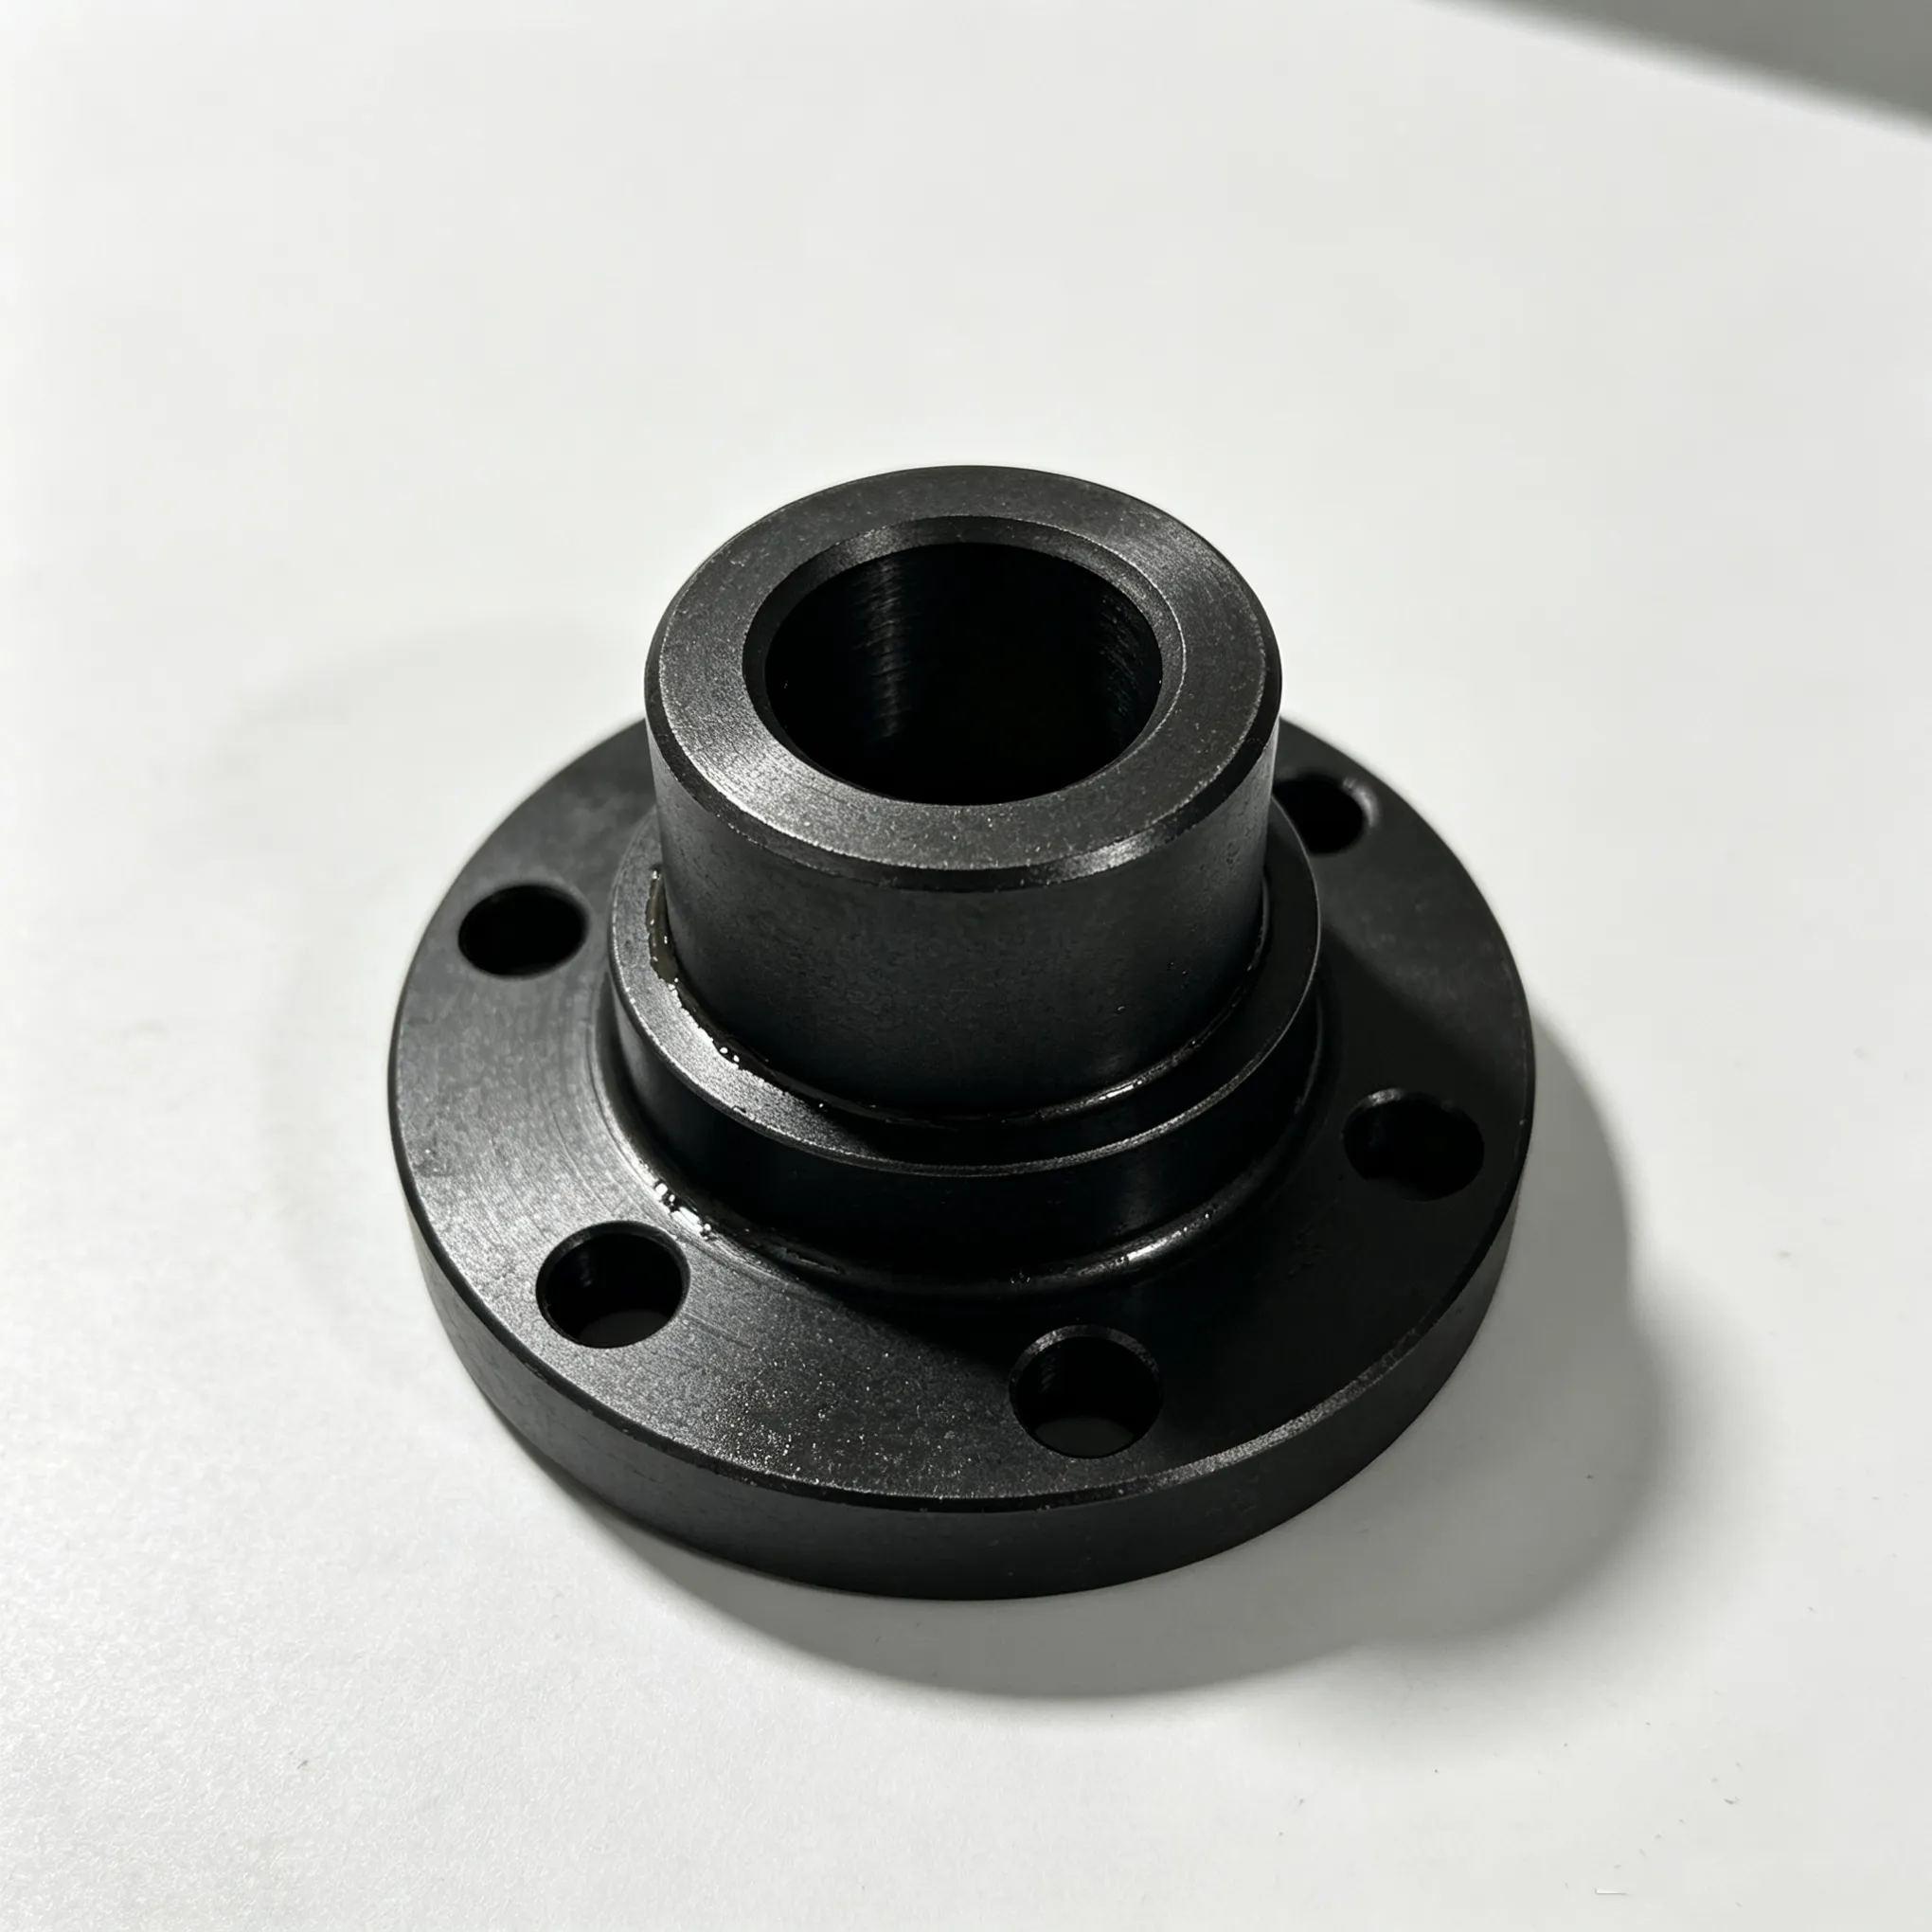
Choosing between 303, 304, 316 and 17-4 for a CNC part is a three-way trade: machinability, corrosion resistance and strength. 303 is the free-machining pick for turned fittings and bushings, 304 the general-purpose washdown grade, 316 the molybdenum-added grade for chloride and salt-spray exposure, 17-4 the strength pick. If you are a design or process engineer at a hardware startup or equipment maker specifying custom stainless parts, that one-liner starts the decision — the sections below finish it.
This page gives the mechanism behind each grade, a quick-selection table, and a checklist mapping your part's environment, loads and quantity to a starting callout. It is not written for commodity bar-stock purchasing, welded sheet-metal fabrication, or service governed by standards your part must certify against. A drawing and a quote settle the rest; nothing here commits you to a purchase.
The decision you are actually stuck on
1. You are the design or process engineer who owns the material callout, so the grade question lands on your drawing first.
2. A stainless part has just left CAD, or its first quote has come back, and the drawing needs a grade.
3. Datasheets give compositions and typical properties, but nothing maps them to your part's environment, features and quantity.
4. The grade gets picked late or swapped after the first quote, which may force a re-quote and a drawing revision.
5. The part may corrode in service, machining may overrun budget, or the release may slip during rework.
6. Run the comparison and checklist below, and record the answers before locking the callout.
What you are trading off when you pick a grade
Machinability, corrosion resistance and strength pull in different directions, and no single grade wins all three.
Machinability is about chips. Grades that break chips short cut faster, finish cleaner and go easier on tools; grades that work-harden and cut gummier usually run slower. That single difference is why the free-machining 303 and the general-purpose 304/316 can quote very differently on the same geometry.
Corrosion resistance is about the environment. All four form the passive chromium oxide layer that makes them stainless; molybdenum in 316 improves pitting resistance where chlorides concentrate, and 17-4's behavior depends on the condition it is supplied in.
Strength is about load: 17-4 is the precipitation-hardening grade for structural parts; the 303/304/316 family usually serves where strength is secondary.
The four grades, mapped to real applications
303: sulfur-added machinability for fittings and bushings
303's sulfur addition is what breaks the chips short, so high-volume turned fittings, bushings, spacers and shafts usually machine faster and finish cleaner in 303 than in 304. The same inclusions can slightly reduce corrosion resistance, which is why 303 usually stays in mild or washdown-type service.
304: the general-purpose washdown grade
304 is the default stainless for machined parts: balanced general corrosion resistance, wide availability, and a long record in washdown service. It work-hardens and cuts stringier, so it usually machines slower than 303 — a difference that can show up in the price on complex or high-volume parts. Start here when the environment matters more than machining time and chlorides are not in the picture.
316: molybdenum for chloride and salt-spray environments
316 adds molybdenum, and molybdenum's job is pitting resistance. Where chlorides concentrate — salt spray, coastal air, chemical exposure — 316 usually resists pit initiation better than 304, and machines a little harder too. The common mistake runs both ways: 316 everywhere can inflate machining time on chloride-free parts, while 304 chosen to save machining time risks pits in service.
17-4 PH: where high strength is required
17-4 PH is the precipitation-hardening grade specified where a part carries real structural load; its strength, machinability and corrosion behavior all depend on the condition it is supplied in. 17-4 is often specified where high strength is required; confirm condition/heat treatment with your supplier. State the required condition on the drawing rather than leaving it implicit: the same bar in different conditions cuts and performs differently. ProLathe lists 17-4 among its machining materials; the heat-treatment question is one for your supplier.
Whichever grade you lock in, stainless parts commonly leave the shop passivated — a treatment that removes surface free iron and supports the oxide layer, and one ProLathe offers in house. Passivation supports the surface's own oxide layer; it does not upgrade one grade into another, so passivated 304 is still 304 in salt spray.
Quick selection, then the checklist
A grade that machines well can still be the wrong grade if the environment corrodes it, so match the row to your environment first and your machining reality second.
| If your part… | Start with | Why |
|---|---|---|
| Is a turned fitting, bushing or spacer made in quantity, in a mild environment | 303 | sulfur-added machinability keeps cutting time down |
| Sees general corrosion or regular washdown | 304 | the general-purpose default |
| Sees chlorides, salt spray, coastal air or chemical exposure | 316 | molybdenum improves pitting resistance |
| Carries structural load and needs high strength | 17-4 | the strength pick; confirm condition/heat treatment with your supplier |
Then confirm the starting point against the part:
Environment → fresh water, washdown, chloride or salt spray, chemicals: ______
Strength requirement → general purpose or structural load: ______
Part style and quantity → high-volume turned or low-volume prismatic: ______
Dominant risk → corrosion in service or machining time at quotation: ______
Condition, 17-4 only → stated on the drawing; supplier confirms heat treatment: ______
Finishing plan → passivation after machining: yes / no
Starting grade to confirm with supplier → ______
What this comparison cannot tell you
No checklist substitutes for a corrosion or materials review when service is aggressive, regulated or certified. The comparison ranks where each grade tends to fit; it does not qualify a part for regulated service or price the machining. Stock, workload and certificates all shift the practical answer, which is why the checklist ends in a starting grade, not a final specification.
For reference, ProLathe's confirmed capabilities:
Stainless steel 303, 304, 316 and 17-4 on the confirmed materials list
CNC turning and milling to ±0.05 mm standard working tolerance
In-house surface finishing: anodizing, QPQ, sandblasting, passivation, painting
Material certificates on request
Quotations within 24 hours
ISO 9001 certified
Run the checklist before you lock the callout
Run the grade-selection checklist on your part and record the environment, strength and quantity answers before you lock the callout. The record takes minutes in CAD and heads off the two expensive failures: a grade swap after quotation, a corrosion surprise in the field.
Two follow-ups depending on where the decision lands:
Recording those answers is the whole action this page asks of you: it turns "which stainless should I use" into a defensible callout attached to the drawing, ready for any supplier to quote.