Oct 10, 2026CNC Machining Tips
CNC Machining Tolerances: What ±0.05 mm Actually Requires from Your Drawing
What a ±0.05 mm tolerance actually requires from your CNC drawing — where tight bands belong, what they demand in process and inspection, and where to open up.
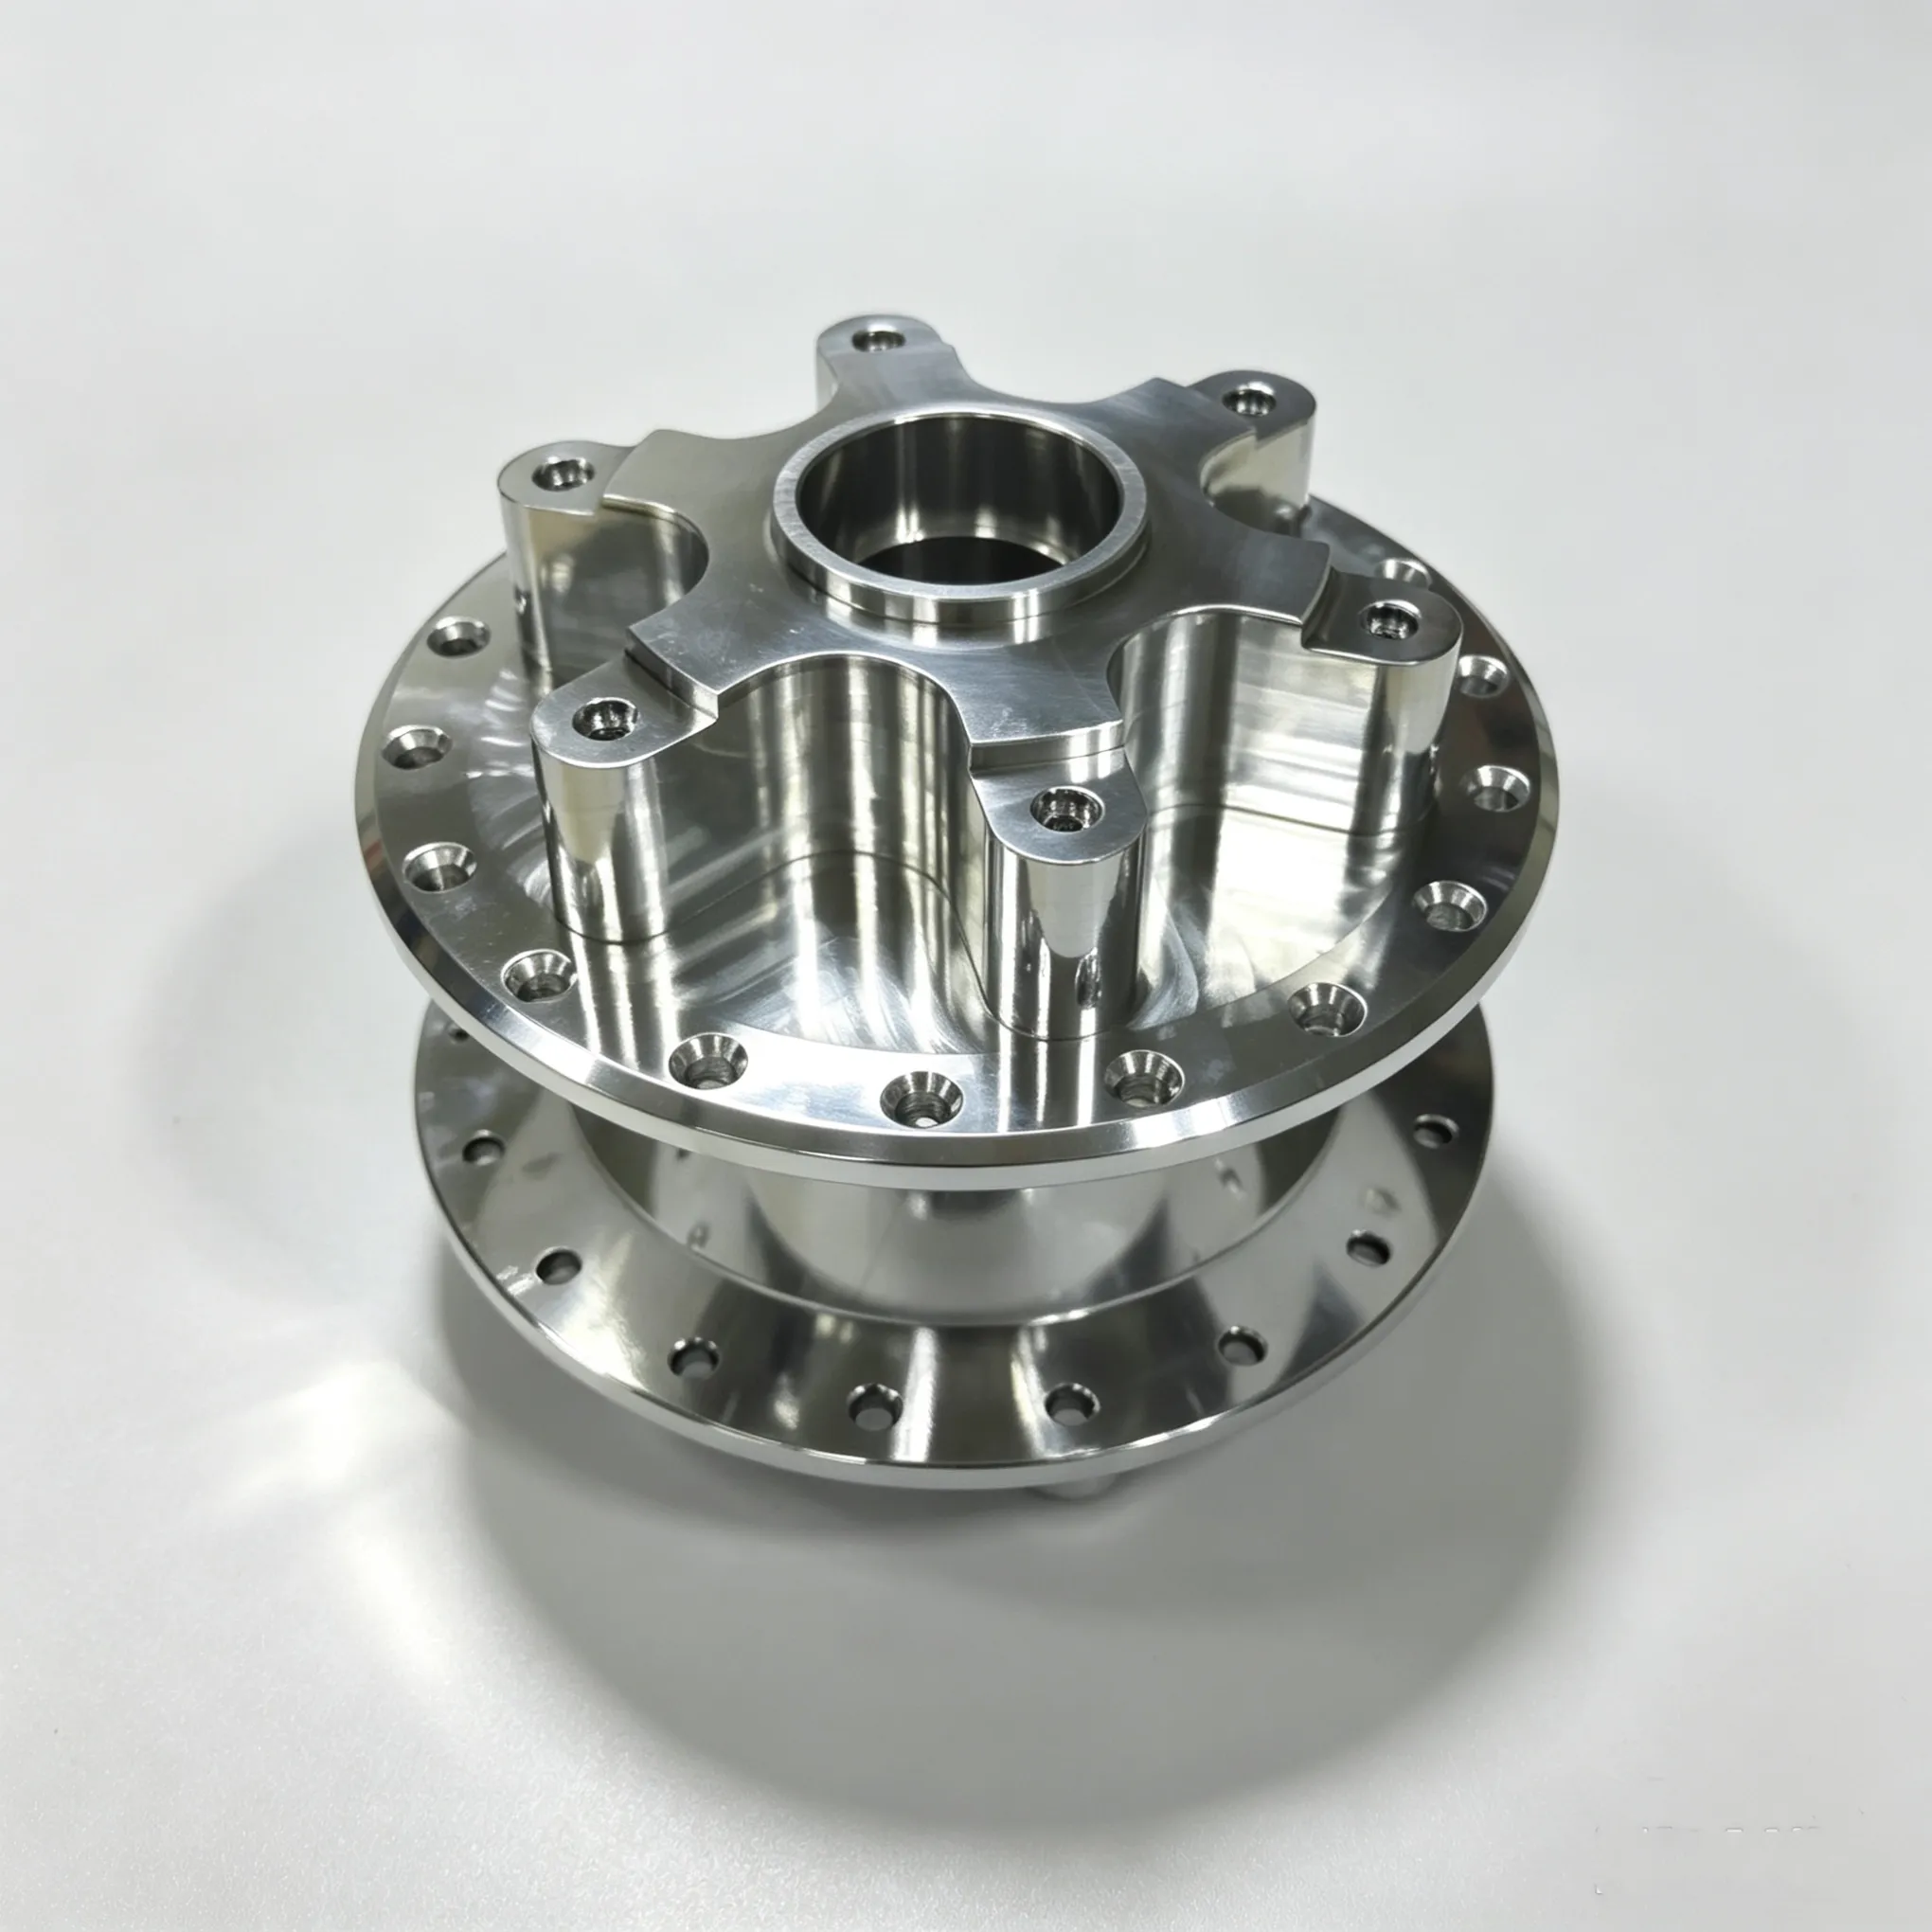
A tolerance on a CNC drawing is not a label. It is a set of instructions: how the part has to be held, which features the machine has to hit, and how the finished part will be measured. If you are a design or process engineer at a hardware startup or equipment maker who dimensions custom metal or engineering-plastic parts, reading those instructions clearly is what keeps quoting and inspection uneventful.
This guide covers what a tolerance band demands in process and inspection, what ±0.05 mm — the standard working tolerance — means in practice, and how to decide where tight bands belong. It is not a GD&T tutorial, a high-volume statistical tolerancing method, or a path to regulated-industry qualification. Nothing here commits you to a purchase; how a specific drawing gets produced is settled when it is reviewed.
The decision you are actually stuck on
1. You are the design or process engineer who owns the drawing, so every tolerance callout on it is yours to defend.
2. The part is heading out for quotation, or a supplier has come back asking which tolerances are actually critical.
3. The drawing carries a mix of bands — some tied to function, some inherited from a template — and nothing records which is which, or where the standard working band already covers you.
4. Guessing may buy a clarification loop, a re-quote, or a drawing revision after the first quote lands.
5. The schedule may slip while the drawing is reworked; over-tight bands may add process and inspection work to every part, and a loose functional band risks parts that fail to fit or seal at assembly.
6. Go through the checklist below and mark every callout functional or default before the drawing leaves your desk.
What a tolerance band actually requires
A band is a commitment the shop keeps on every part, not a target it hits once. The question is not whether it can be held but what holding it changes in cutting, fixturing, and measurement.
On the machine
Cutting tools wear, so a process holding a band has to compensate as parts accumulate, and how the part is referenced on each setup decides where the band is actually achievable. That is true at ±0.05 mm, and more so as bands tighten. At the standard band the work is routine — it sits inside what a maintained process does by default on ordinary features. Tighter than that, each step asks the process for more: more careful setups, slower finishing passes, and a plan for how the band survives from first setup to last. How much more is a per-part question.
At inspection
A tolerance is only as good as the measurement behind it. A band tighter than the standard one may demand instruments chosen to resolve it, parts settled to a stable temperature before measuring, and more dimensions verified per part — checks may stretch from sampling toward every-part inspection. None of that argues against a tight band where the function needs it; it argues for keeping only the bands that are there on purpose.
±0.05 mm as the standard working band
ProLathe machines to ±0.05 mm as its standard working tolerance. On a typical part, dimensions left at the standard band are held by the normal process — the way the shop sets up, cuts, and verifies by default. No special plan attaches to them.
Standard does not mean every feature is fine at ±0.05 mm; it means ±0.05 mm is the default. Features whose function needs more than the standard band are planned case by case — the callouts on the drawing drive the process, not the other way around. The habit: treat the standard band as what the part gets without asking, and every tighter band as something the process has to earn.
Where tight tolerances belong — and where they don't
The features that earn tight bands are the ones where function breaks when the number moves: a shaft that has to slide in a bore without play or binding, a seal groove that has to keep sealing, a bearing seat whose size sets the fit. A tight band belongs only where the function fails when the dimension drifts — a fit, a seal, or a running surface — and everything else defaults.
Everything else usually defaults. Faces nothing mates against, clearance holes that only need the fastener through, purely visual surfaces — a band carried by habit adds no control, only process care and inspection work on every part.
How material and geometry change the callout
Thin or slender sections may relax once clamping pressure releases, so a tight band on them may take stress-relieving and lighter finishing passes — or may be the wrong call entirely.
A feature cut across more than one setup inherits every re-fixture; it holds only as well as the part is re-referenced.
Polymers move: temperature shifts dimensions, and nylon in particular may drift with moisture uptake, so a band verified at the machine may read differently in service.
The same callout may be routine on one alloy and demand more care on another; machinability is part of what a band costs.
The functional-or-default checklist
Work through the drawing feature by feature, filling each field as you go:
Tolerance callouts on the drawing → list each feature with its band: ______
Callouts tied to a fit, seal, or running surface → mark each one functional: ______
Callouts with no function you can name → mark each one default: ______
Features whose function fails if the dimension drifts → confirm the band matches the function: ______
Faces where the standard working band is enough → leave at default: ______
Bands tighter than the standard band → write the reason each one exists: ______
Verification per tight band → how it will be measured, and at which stage: ______
Callouts to open up before quotation → your default candidates: ______
What this checklist cannot tell you
The checklist sorts callouts into functional and default; it cannot tell you what any band will cost to hold on a specific shop's machines. That is a per-drawing question, settled at review and quotation. What the checklist does give you is a drawing whose bands all answer to function — so the conversation starts from what the part has to do, not from habit.
For reference, ProLathe's confirmed capabilities:
CNC machining to ±0.05 mm standard working tolerance
Production organized around the tolerance callouts on your drawing
Drawing review before every quotation (DFM-first review)
ISO 9001 certified
Run the checklist on your own drawing
Run the functional-or-default checklist on your drawing and mark every tolerance callout before it goes out for quotation. The marking takes minutes in CAD; the alternatives are a clarification loop, a re-quote, or a part that misses its function at assembly.
Two follow-ups, depending on where the marking lands:
Once the bands are sorted, state tolerances clearly in a quotation-ready drawing so the quote matches the function.
Recording which callouts are functional and which are default is the whole action this page asks of you. It turns "what tolerance does this part need" into a list that travels with the drawing — and every later conversation about the part starts from function.