Oct 10, 2026CNC Machining Tips
Threads and Tapped Holes in CNC Parts: Depth, Callout and Failure Guide
How to design and call out threads and tapped holes for CNC parts — depth ratios, blind versus through holes, and the failure modes to design around.
Most thread problems on CNC parts are specified on the drawing, not caused at the machine. A callout that leaves pitch, class, or depth to assumption can come back as a broken tap, a short thread, or a fastener that will not seat. If you are a design or process engineer at a hardware startup or equipment maker who puts tapped holes on machined parts, a short pass over your callouts will usually show you which holes carry those risks.
This guide covers the four elements a complete thread callout needs, the commonly used rule of thumb for engagement depth, and the blind-versus-through decisions. It is not written for fastener standards work, high-volume production planning, or threads governed by a specification you cannot change. Nothing here commits you to a purchase.
The decision you are actually stuck on
1. You are the design or process engineer who owns the drawing, so a thread failure or an assembly stoppage lands on you first.
2. A part with tapped holes — blind ones especially — has just left CAD and is heading for quotation.
3. The callouts name a size, but nothing says whether pitch, class and depth are complete, or what clearance the tap needs in a blind hole.
4. The gaps surface late — a DFM question, a broken tap at the shop, a fastener that will not engage — and each may force a drawing revision.
5. The release may slip while holes are re-detailed or parts are scrapped and remade.
6. Walk every threaded hole through the checks below and complete the ambiguous callouts before the part is quoted.
What a complete thread callout includes
A callout that names the thread size but omits pitch, class, or depth is not a complete callout — it is an assumption you have asked the shop to make for you. Four elements matter.
Nominal size and pitch
A nominal size alone does not define a thread: the same diameter can carry different pitches. Leave the pitch off and the shop may assume a common one, and your fastener may not fit the hole it receives. State the pitch (or threads per inch) explicitly, even when it is the pitch you consider standard.
Thread class
The class states how loose or tight the mating threads fit. Leave it off and the shop will usually assume a general-purpose class, which is fine for most fastening. Call one out deliberately when the function needs it — smooth adjustment, or resistance to loosening — and a tighter class may add gaging or inspection effort.
Depth, drill depth and hole type
State how deep the usable thread must run and, for a blind hole, how deep the drilled hole runs below it — clearance that gives the tap room to enter and the chips somewhere to go. Also mark the hole as through or blind explicitly: it is the distinction that changes everything downstream, and the one most often left ambiguous when copied from a similar part.
How deep should threads engage
A commonly used rule of thumb sizes engagement depth as a multiple of the nominal thread diameter, adjusted for the materials joined — softer ones usually need more engagement for the same load. Treat it as a starting point, not a standard to enforce: the multiplier that fits a static joint may not fit a cyclic one, or your case at all. Past a certain depth, added engagement usually buys little strength: the load concentrates in the first few threads. And in a blind hole, every increment of engagement you demand is depth the tap has to survive.
Blind versus through, and the failures to design around
The through-versus-blind decision drives most of the machining risk in a threaded hole.
Through tapped holes
A through hole lets the tap exit, clears chips naturally, and carries full thread end to end. If the function allows it, the machining risk usually drops — a blind hole should be blind for a reason.
Blind tapped holes: the tap needs room at the bottom
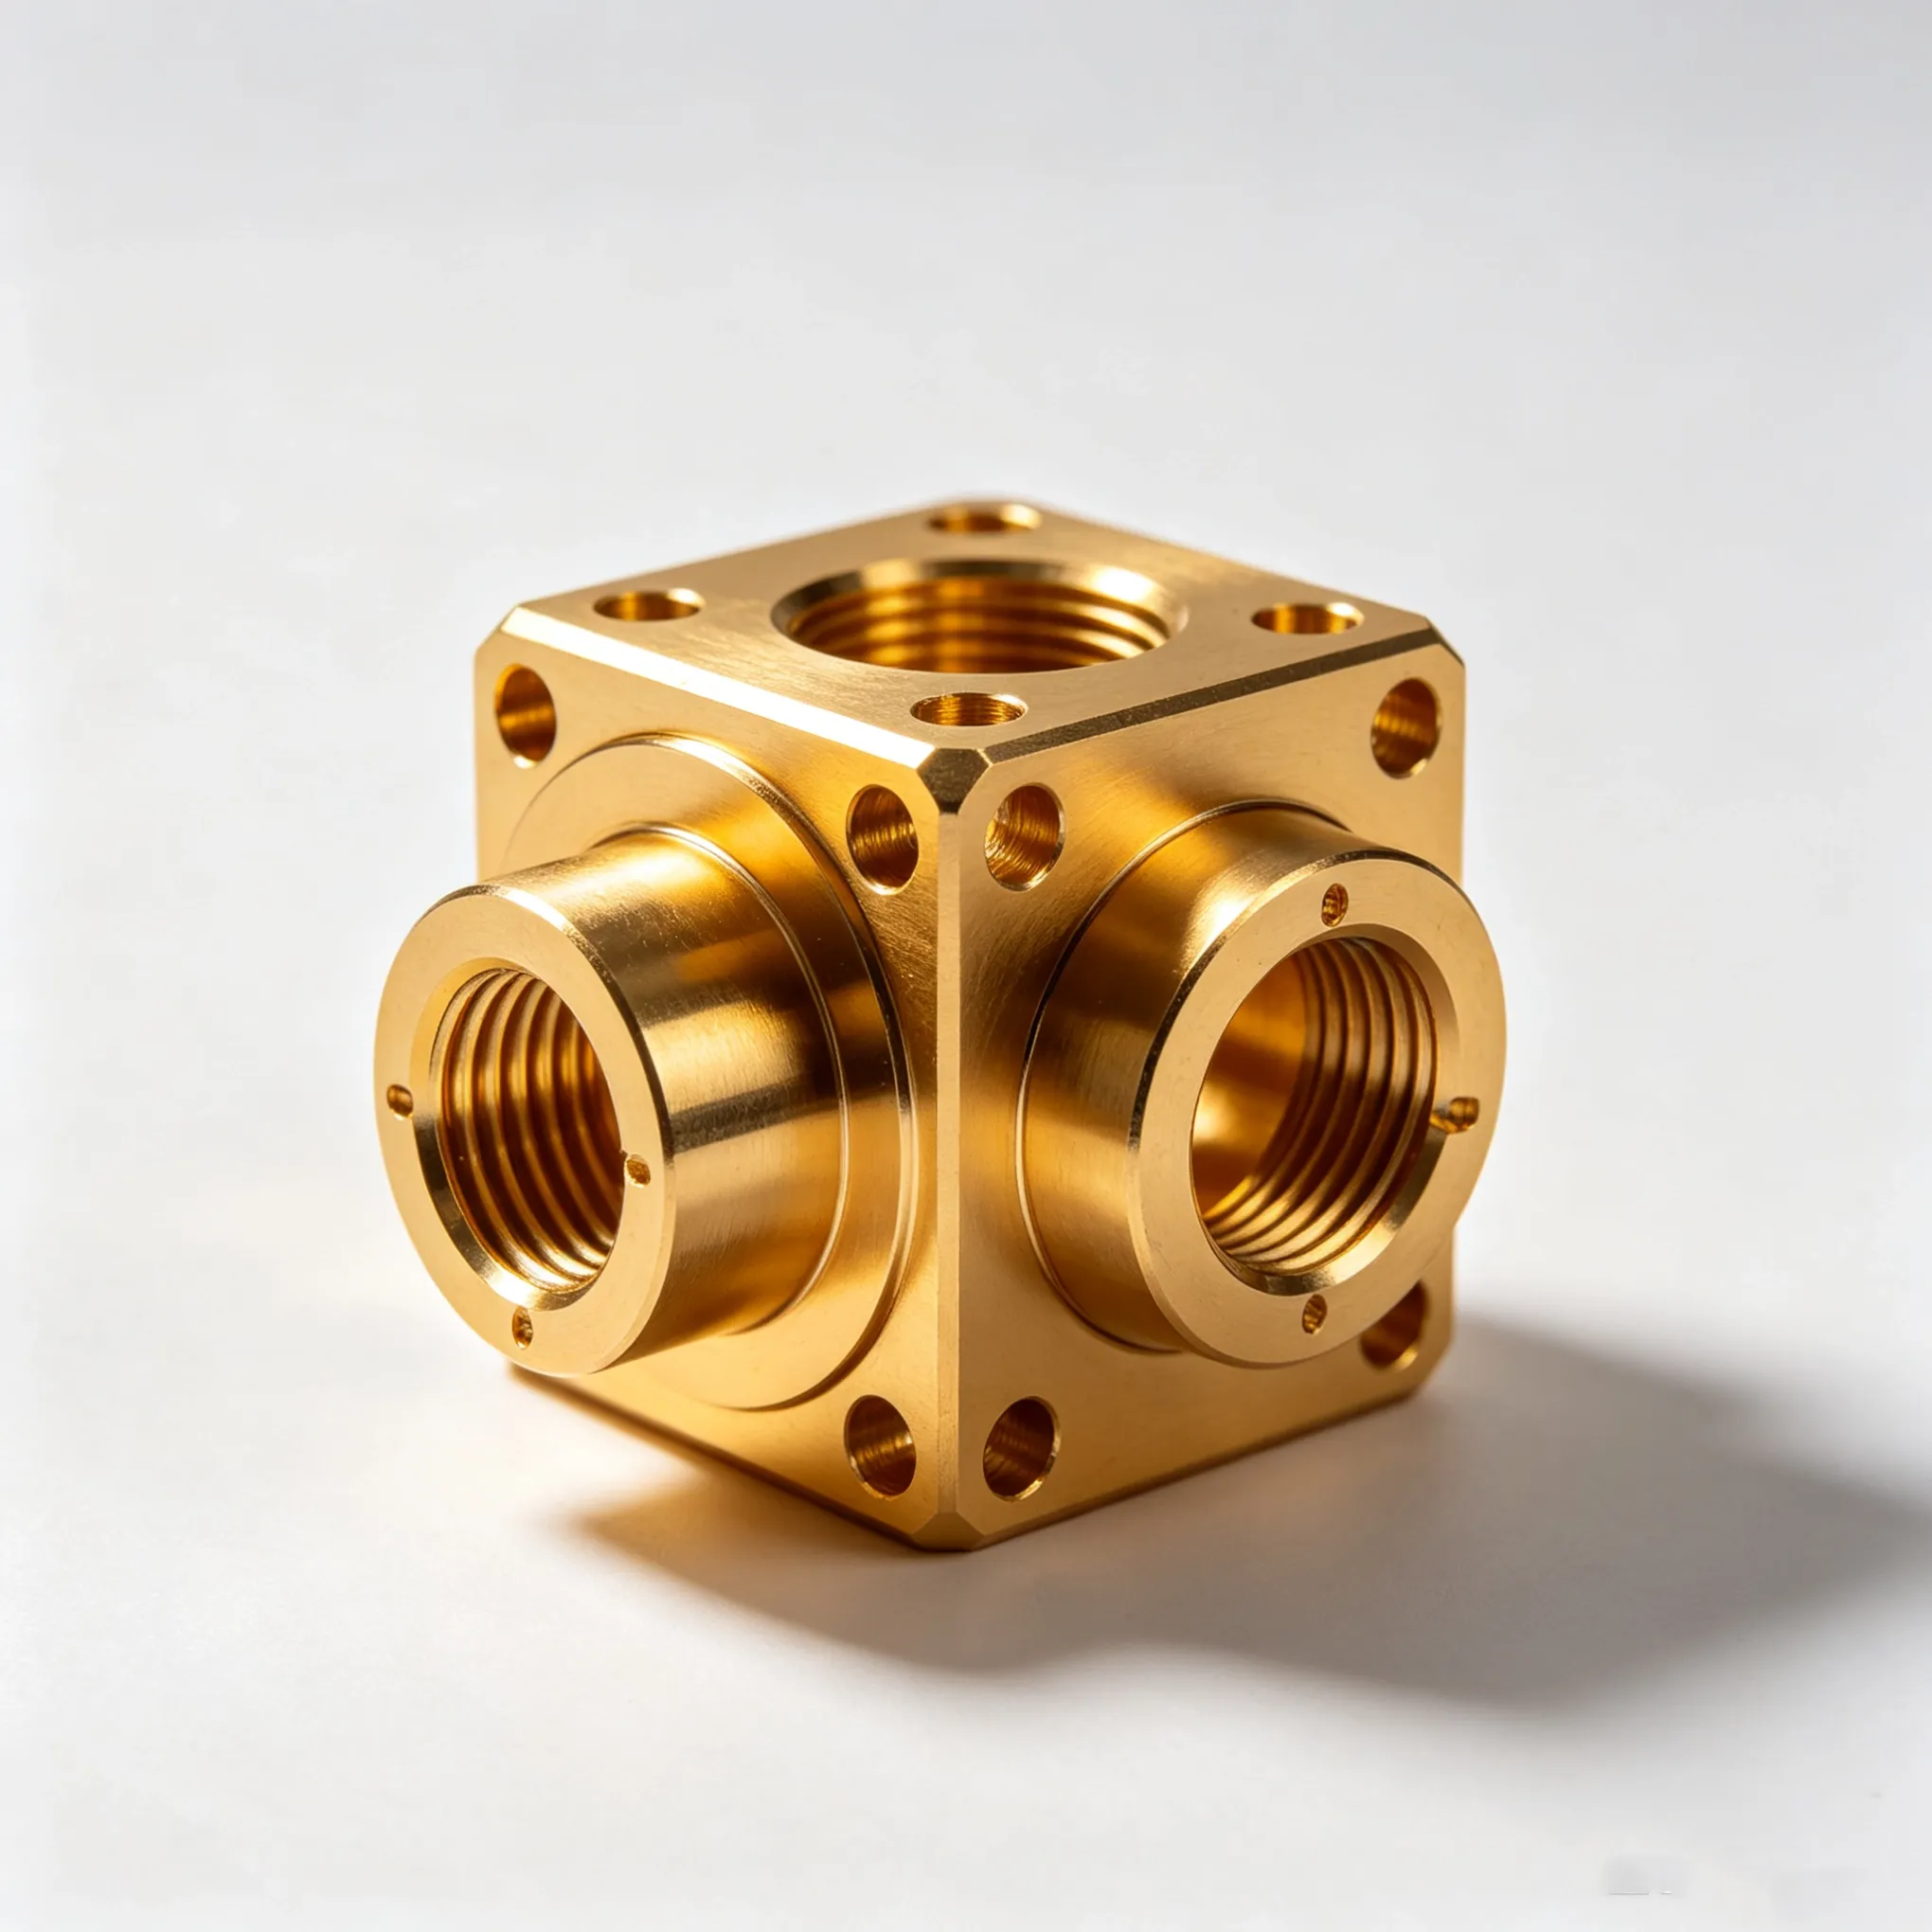
In a blind hole the tap cannot exit, so the drilled hole must run deeper than the full thread depth — clearance that keeps the tap from bottoming out. A blind hole that demands usable thread almost to the bottom leaves the tap nowhere to go, and that is where taps most often break. When the design genuinely needs thread close to the bottom, say so deliberately and expect the question at DFM review.
The failure modes to design around
Three recur on machined parts. Broken taps: over-deep, undersized blind holes are the usual suspects, and one can scrap a nearly finished part. Thread runout at a shoulder: a tap cannot cut full thread against an adjacent face, so provide a relief groove or extra depth; where the drawing is silent, the fastener may stop short and the assembly may not close. Tapping uses a tap that matches the thread form, while thread milling uses a smaller rotating tool — the route is the shop's process decision, so define the thread clearly enough that either route can be evaluated.
The thread callout self-check
Run this checklist for every distinct threaded hole and fill in what you find:
Hole type (through / blind) → which is it, and why: ______
Size and pitch → both stated: yes / no
Thread class → stated, or shop default consciously accepted: yes / no
Full-thread depth → stated: ______
Drill depth below thread → stated for blind holes: ______
Engagement depth → rule-of-thumb starting point, not enforced standard: yes / no
Shoulder interface → relief groove or clearance provided: yes / no
Through-hole candidates → blind holes that could be through: ______
Fixes before quoting → callouts to complete: ______
What this checklist cannot tell you
The checklist catches ambiguous callouts; it cannot guarantee how any specific hole will machine. Tap behavior depends on the shop's tooling, the material and each hole's depth-to-diameter situation — suppliers weigh those differently. Treat the checklist as a way to remove ambiguity before quotation, not as a prediction of outcomes.
For reference, ProLathe's confirmed capabilities:
CNC turning and milling to ±0.05 mm
Materials including aluminum 6061/7075, steel, stainless steel, brass and bronze
DFM-first review of every drawing before quotation
Quotations within 24 hours
ISO 9001 certified
Run the checklist on your own drawing
Run the thread callout checklist on your own drawing and mark which holes need a complete callout before you request quotes. The fixes are often minutes in CAD; discovering them at first article costs a revision loop and may cost scrapped parts.
Two follow-ups depending on where your check lands:
Once the callouts are complete, call out threads clearly on the drawing as part of the full quotation-ready package.
When a hole needs unusually deep threads, see why deep threads add cost before you lock the depth in.
Running the checklist and marking the callouts to complete is the whole action this page asks of you.